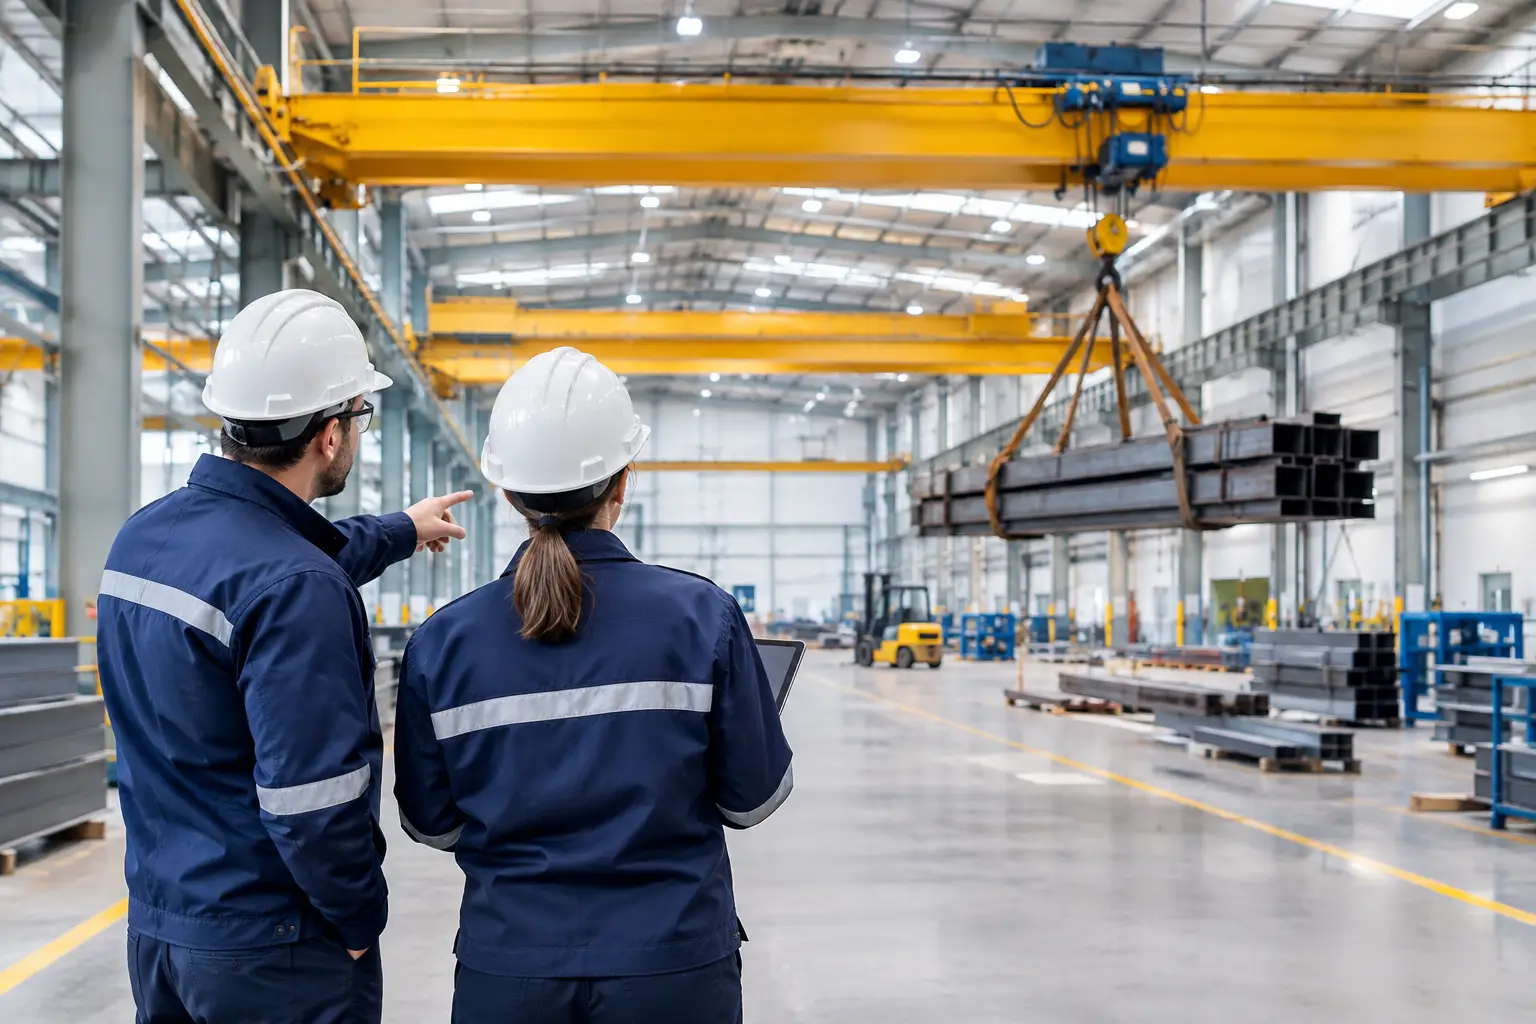
A crane can have the correct lifting capacity and still create a production bottleneck. The usual cause is not the hoist itself. It is the path the load must travel, the areas it cannot reach, or the workstations forced to wait for access. Well-engineered factory crane layouts treat lifting as part of the production flow, not as an item added after the building is complete.
For plant managers, project engineers, and maintenance teams, layout decisions affect far more than the initial equipment price. They determine operator safety, usable floor area, installation complexity, maintenance access, and the downtime risk carried by the operation for years to come.
Start With the Material Flow, Not the Crane
A practical layout begins by following the material through the facility. Identify where goods arrive, where they are staged, where they are processed, where they need to be turned or positioned, and where they leave. This reveals the actual lifting routes that equipment must support.
For example, a fabrication shop may receive steel near one end of the building, move it to cutting and welding stations, then transfer finished assemblies to inspection and dispatch. A single overhead crane runway may serve the length of the shop efficiently. In another facility, frequent lifts may occur only within individual work cells. Several jib cranes or workstation cranes can be a better fit than a larger system covering unused space.
The key question is not simply, “How much can we lift?” It is, “Where must the load be picked up, carried, positioned, and released without interfering with people, machinery, or other material movement?” A layout that matches these answers reduces unnecessary handling and waiting time.
The Core Decisions in Factory Crane Layouts
Every crane layout is shaped by several connected engineering decisions. Capacity matters, but it is only one part of the system.
Coverage and hook approach
The crane must provide useful hook coverage across the required working area. This includes more than the runway length and bridge span. The hook needs to reach close enough to walls, machines, racking, loading points, and work benches to complete the lift safely.
End approach and side approach dimensions are often overlooked during early planning. These dimensions define how close the hoist can travel to the end of the runway and how close the hook can reach toward either side of the building. A layout may look adequate on a drawing yet leave a critical machine loading point just outside the practical lifting zone.
Travel paths and interference points
A load should travel through a clear, predictable route. Place crane runways so lifted materials do not routinely pass over occupied workstations, offices, pedestrian routes, or sensitive equipment. Where crossings cannot be avoided, the facility should establish controlled operating procedures and clear exclusion areas.
Consider the equipment already on the floor. Tall machinery, extraction ducting, conveyors, racks, service platforms, and fire-protection systems can all reduce available clearance. Overhead space must be surveyed carefully before selecting a crane type, lifting height, or runway elevation.
Headroom and lifting height
Required lifting height is measured from the lowest expected load position to the highest point needed for safe transfer. However, the total vertical space required also includes the load, lifting attachments, hook block, hoist dimensions, crane girder depth, and safety clearances.
A low-headroom hoist or a single-girder configuration may preserve valuable vertical clearance. On the other hand, a double-girder crane can provide higher capacity, improved hook height, and better suitability for demanding duty cycles. The right choice depends on the building structure, load profile, and operating requirements rather than a preference for one crane style.
Load capacity and duty classification
Design capacity must account for the heaviest anticipated lift, including below-the-hook devices such as lifting beams, grabs, magnets, or specialized fixtures. It should also reflect realistic future requirements. Installing a crane with little capacity margin can limit production changes or require expensive replacement when product sizes increase.
Capacity alone does not define the equipment. A crane used occasionally for maintenance has different mechanical and electrical demands than one operating continuously across multiple shifts. Lift frequency, travel distance, load spectrum, speed requirements, and operator control method all influence the appropriate duty classification and component selection.
Choose a Layout That Fits the Building and the Work
Overhead traveling cranes are often the strongest option when a facility needs broad coverage without consuming floor space. They are particularly effective for moving heavy materials along a production line, between bays, or from storage to processing areas. Their runways may be supported by the building structure or by independent columns, depending on the facility and structural assessment.
Jib cranes suit localized, repetitive lifting near machines, assembly benches, loading stations, and maintenance areas. They can reduce reliance on a central overhead crane for smaller routine tasks. A jib crane is not automatically the lower-cost answer, however. Multiple units may create overlapping operating zones, installation constraints, and maintenance requirements that need to be considered together.
Gantry cranes are useful where the building cannot support crane runways or where lifting is required in an outdoor yard. They do require floor-level travel space and well-managed routes, which can be less suitable in congested internal production areas.
For some operations, a combined layout delivers the best result. An overhead crane may handle major transfers and heavy assemblies, while jib cranes serve high-frequency work cells. This keeps the main crane available for work that genuinely requires its coverage and capacity.
Design for Safety at the Same Time as Productivity
A productive lifting layout does not ask operators to work around hazards. It removes predictable conflicts before equipment is installed. Safe clearances, designated walkways, protected work zones, clear sightlines, and appropriate warning devices should be considered during layout development.
Load control is equally important. Long, flexible, or uneven loads may require tag lines, lifting beams, spreader beams, or purpose-designed lifting fixtures. These devices affect the total lifted weight and required headroom, so they must be included in the engineering calculation from the start.
Visibility also deserves attention. An operator needs a clear view of the pickup and set-down points, or reliable communication with a trained signal person where visibility is restricted. Radio controls can offer greater freedom of movement than pendant controls in some applications, but the control method should be selected around the actual work environment and operating procedures.
Plan for Installation and Maintenance Access
The best layout on paper can become costly if it ignores how equipment will be installed, inspected, and serviced. Runway supports, electrical supply routes, access platforms, and future replacement paths should be planned early. Retrofitting these provisions after construction is often more disruptive than making room for them during the design stage.
Maintenance access is particularly important around hoists, gearboxes, brakes, motors, festoon systems, and end carriages. Equipment should be positioned so technicians can inspect and service critical components without creating unnecessary production shutdowns or unsafe work conditions.
Local availability of common spare parts also supports the layout decision. A customized crane system should remain serviceable throughout its working life, with components selected for the operating environment and a practical maintenance plan established from commissioning onward.
Common Layout Mistakes That Create Long-Term Cost
Several errors appear repeatedly in factory projects. The first is designing around the building shell without studying material flow. Another is selecting capacity based only on today’s largest load while overlooking lifting attachments, future products, or operating duty.
A third mistake is treating every square foot as production space and leaving no room for safe load travel, maintenance access, or staging. Congestion may seem efficient initially, but it can increase handling time, raise collision risk, and make maintenance more difficult.
Finally, avoid assuming a standard crane arrangement will suit a nonstandard process. Existing columns, roof geometry, machine locations, floor conditions, and utility services often require a tailored approach. A site assessment and coordinated engineering review are usually less expensive than correcting a poorly placed runway after production has started.
Build Flexibility Into the Layout
Production requirements rarely stay fixed. Where future expansion is likely, consider extending runway length beyond the immediate work area, allowing for a second hoist, reserving electrical capacity, or keeping adjacent space clear for later process changes. Not every project needs this allowance, and budget discipline matters. The decision should be based on a realistic expansion plan rather than a vague desire to future-proof everything.
At MFEI, the objective is to translate operational requirements into a lifting system that fits the site, budget, and expected service life. That means examining the building and workflow together, then selecting equipment and support arrangements that can be installed, maintained, and relied upon in daily operation.
A factory layout earns its value when the crane becomes an uncomplicated part of the workday: available when needed, clear of the work when not, and designed around the people and materials that keep the operation moving.