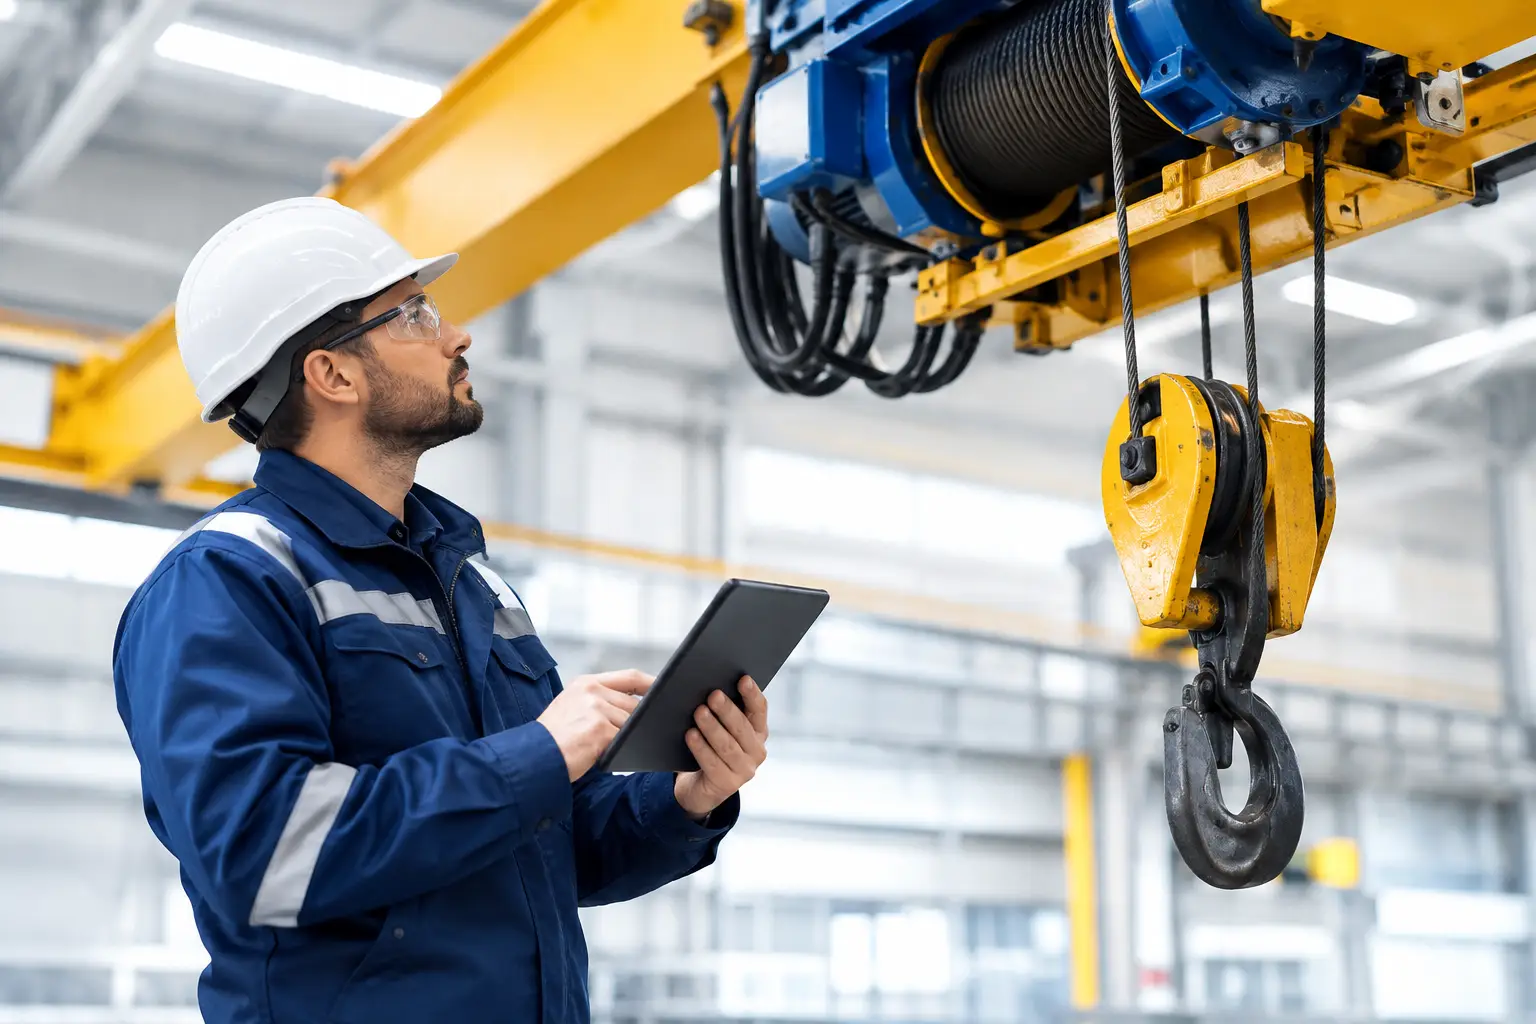
A hoist rarely fails at a convenient time. A brake that begins slipping, a worn wire rope, or an overheating motor can stop a production line, delay a loading operation, and put people at risk long before a complete breakdown occurs. Predictive hoist maintenance gives maintenance teams a practical way to identify those warning signs early and plan corrective work before lifting availability is affected.
For facilities that depend on overhead cranes, monorails, winches, and electric chain hoists, the aim is not to replace routine servicing. It is to make service decisions more informed. By combining inspections, operating history, and condition data, plant teams can focus attention on the components most likely to cause disruption or create a safety concern.
What Predictive Hoist Maintenance Means in Practice
Predictive maintenance uses the actual condition of equipment to help determine when maintenance should be performed. Rather than changing or rebuilding components only because a calendar interval has passed, the maintenance plan responds to measurable deterioration, abnormal performance, and operating conditions.
With a hoist, this approach may involve tracking brake performance, motor current, gearbox noise, hook condition, rope or chain wear, limit switch function, and the number and type of lifting cycles completed. A technician then interprets the findings in the context of how the equipment is used. A hoist that handles light loads occasionally will have different service needs from one that repeatedly lifts near its rated capacity through multiple shifts.
The distinction matters. Calendar-based preventive maintenance remains necessary for lubrication, safety checks, statutory inspection requirements, and basic adjustment. Predictive work adds a condition-based layer that helps a facility avoid unnecessary replacement while reducing the chance that a developing defect becomes an emergency repair.
Why Hoists Benefit From Condition-Based Service
A hoist is a system of connected mechanical and electrical components. When one component begins to degrade, the effect can spread. A brake that does not release cleanly can increase motor load. Poor gearbox lubrication can accelerate gear wear and raise operating temperature. Misalignment can cause uneven rope spooling, which shortens rope life and affects safe lifting performance.
The most valuable benefit of early detection is planning. A maintenance manager can schedule a brake adjustment, rope replacement, bearing change, or control repair during a planned shutdown instead of reacting after an unexpected stoppage. Procurement teams gain time to obtain the correct parts, and operations teams can arrange an alternative lifting method where required.
This is especially relevant where a single crane or hoist serves a critical work cell, maintenance bay, dispatch area, or production process. The cost of downtime may be far greater than the cost of a scheduled inspection or component replacement. Predictive maintenance supports cost discipline because it directs resources toward genuine equipment condition, not assumptions.
The Components That Need Closer Attention
Not every hoist requires advanced sensors on every component. The right level of monitoring depends on the hoist duty classification, load profile, environment, equipment age, and consequence of downtime. However, several areas consistently deserve close technical attention.
Brakes and Load Control
The hoist brake is central to safe load holding. Changes in stopping distance, delayed engagement, unusual noise, heat buildup, or inconsistent holding behavior should be investigated promptly. Brake wear does not always present as an obvious failure. A qualified technician can measure wear, verify air gaps or settings where applicable, inspect friction surfaces, and confirm proper operation under controlled conditions.
Wire Rope, Load Chain, and Hook Assembly
Wire rope and load chain are exposed to repeated stress, wear, contamination, and possible misuse. Inspections should look beyond visible damage. Technicians assess lubrication condition, broken wires, abrasion, deformation, corrosion, chain elongation, twist, and the way the rope tracks through the drum and sheaves.
The hook assembly also requires attention to throat opening, twist, cracks, latch condition, and bearing movement. These are direct safety items, not parts to defer because the hoist is still running.
Gearbox, Bearings, and Lubrication
A rising operating temperature, vibration, or change in gearbox sound may indicate lubrication issues, bearing wear, gear damage, or misalignment. Trending these conditions over time is more useful than judging a single reading in isolation. A technician familiar with the hoist model and its normal operating behavior can distinguish between an acceptable operating characteristic and a developing fault.
Motors, Controls, and Safety Devices
Electrical issues are often intermittent before they become disruptive. Motor current trends, contactor wear, pendant response, inverter or variable-frequency drive fault history, cable condition, and limit switch performance can provide early warning. Emergency stops, upper and lower limits, overload protection, and other safety devices must be tested as part of a controlled maintenance program.
Building a Predictive Maintenance Plan That Fits the Site
An effective program begins with an equipment baseline. Record the hoist make, model, capacity, duty, installation date, operating environment, service history, past failures, and available spare parts. This creates a reference point for future inspection findings and helps identify units that deserve more frequent review.
Next, classify equipment by operational criticality. A hoist used to support daily production or handle high-value loads should receive more detailed condition monitoring than an infrequently used unit with an easy backup option. This does not mean lower-criticality equipment can be neglected. It means inspection depth and response time should reflect real operational risk.
A practical program often combines four types of information:
- Visual and functional inspection findings from qualified service personnel
- Usage data, including operating hours, starts, lifting cycles, and load patterns
- Condition indicators such as temperature, vibration, motor current, and brake behavior
- Repair history and recurring fault records
For many facilities, disciplined inspections and accurate records deliver a meaningful improvement before advanced monitoring technology is needed. Sensors can be highly useful on critical or high-duty assets, but they are not a substitute for engineering judgment. A sensor may show an abnormal trend; a competent technician determines the likely cause, urgency, and appropriate corrective action.
Turning Inspection Results Into Better Decisions
Condition data has value only when it leads to clear action. Each finding should be assigned a priority based on safety impact, likelihood of failure, operational consequence, and parts lead time. A worn brake lining may require immediate action if holding performance is affected. A minor oil seep may be monitored and planned for repair during the next shutdown, provided it is not creating an unsafe condition or accelerating damage.
Clear reporting helps maintenance, operations, and procurement work from the same facts. A useful service report identifies the equipment, observed condition, likely cause, recommended action, priority, and parts required. Photographs and measurement records can be valuable where wear progression needs to be demonstrated over several inspections.
This approach also improves budgeting. Instead of treating every repair as an unexpected expense, managers can forecast likely work across the coming quarter or year. Local availability of commonly required spare parts can further shorten repair windows, particularly for items such as brake components, contactors, limit switches, ropes, chains, and control accessories.
Common Mistakes to Avoid
The first mistake is confusing predictive maintenance with occasional inspection. Prediction requires comparison over time. If service reports are incomplete, inconsistent, or filed without review, the facility loses the ability to see trends.
The second is relying on a fixed maintenance interval for every hoist. Time-based schedules are necessary, but they do not account for differences in load spectrum, duty cycle, environment, operator practice, or equipment condition. A hoist in a dusty, humid, corrosive, or high-temperature area may require closer attention than an identical unit in a clean workshop.
The third is delaying corrective work because the equipment remains operational. Many failures develop gradually, and continuing to operate with abnormal noise, poor braking, damaged rope, erratic controls, or recurring overload events can turn a manageable repair into a major outage. Safety-related defects should always be handled according to the equipment manufacturer’s requirements and site safety procedures.
Where Engineering Support Adds Value
Some defects are straightforward. Others require an assessment of loading, structural arrangement, electrical controls, duty classification, and operating practice. This is where an experienced lifting-equipment engineering partner can add value by connecting maintenance findings to the wider material-handling system.
For example, repeated brake wear may indicate excessive cycling or unsuitable control settings. Rope damage may point to drum, sheave, or alignment issues rather than a rope problem alone. Frequent electrical faults may be related to supply quality, pendant handling, cable travel, or an aging control system. Replacing the visible failed part without addressing the cause can lead to repeated cost and disruption.
MFEI approaches service and maintenance as part of the equipment lifecycle, with technical support that can extend from inspection and repair to parts planning, modernization, and site-specific engineering recommendations. The practical objective is dependable lifting performance that suits the facility’s workload, budget, and operational constraints.
A well-run predictive program does not promise that a hoist will never need repair. It gives your team more time, better information, and safer choices when repair is needed. Start with the hoists that would cause the greatest disruption if they stopped tomorrow, establish a reliable condition baseline, and let each inspection build a clearer picture of the equipment your operation depends on.