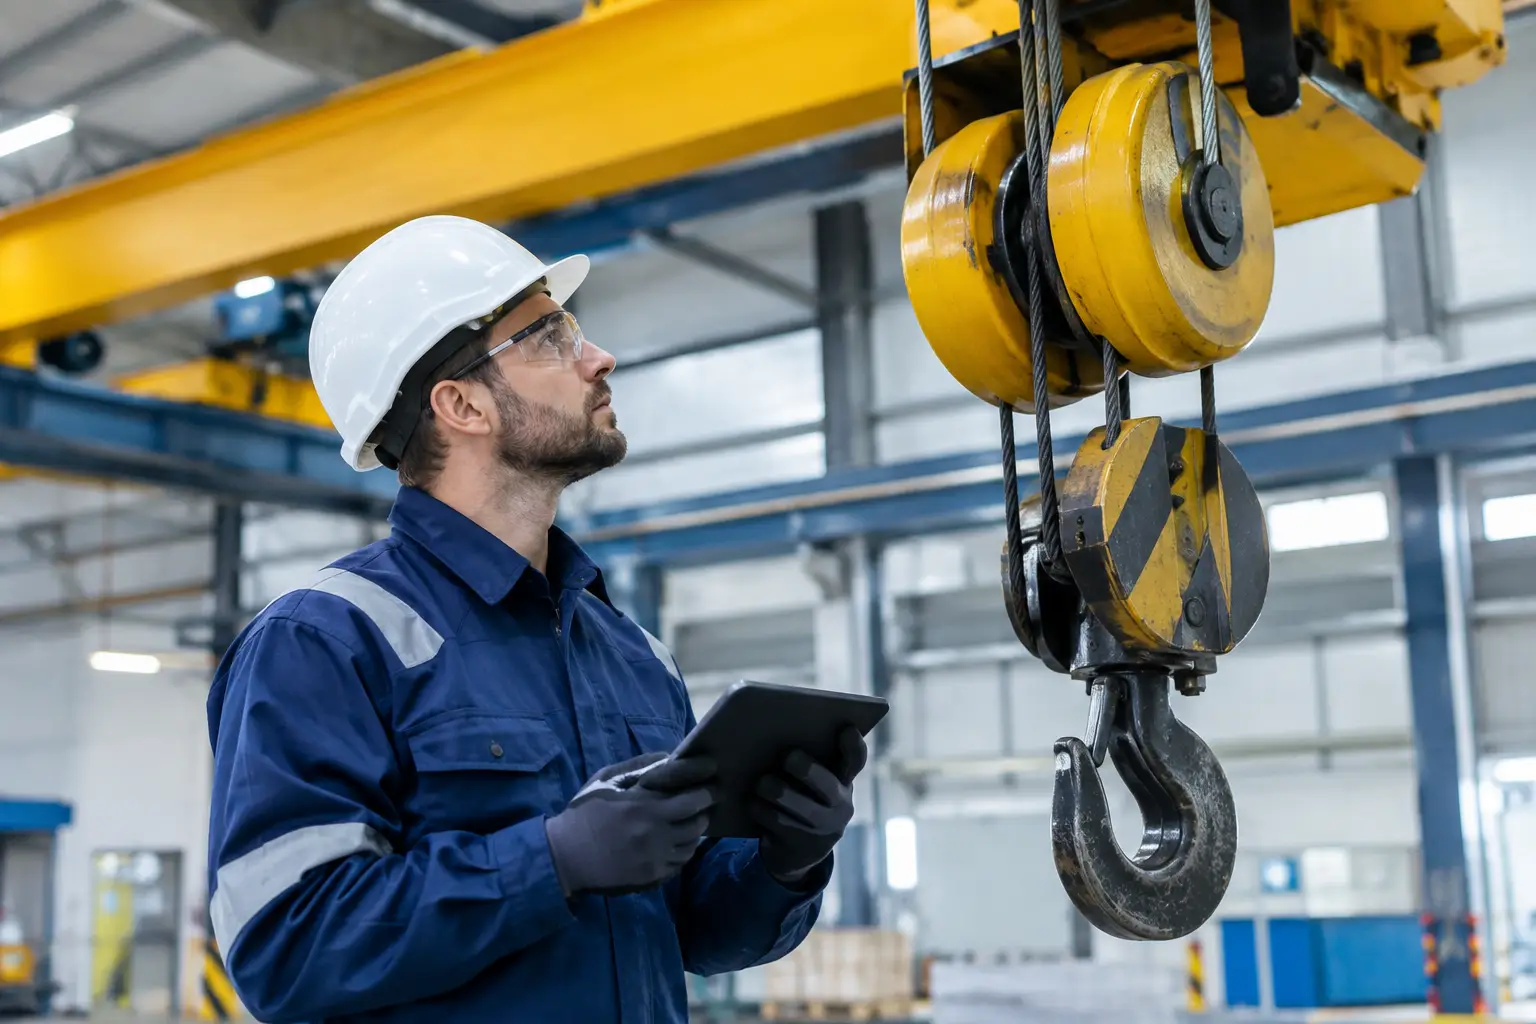
A hoist failure rarely affects only one lift. When a wire rope hoist, chain hoist, or traveling mechanism is unavailable, operators may be unable to feed a production line, load a vehicle, position a tool, or move finished goods. Workarounds can introduce handling delays and safety exposure. Knowing how to reduce hoist downtime starts with treating the hoist as a production asset, not a piece of equipment that receives attention only after it stops.
The most effective approach combines disciplined inspection, planned maintenance, trained operation, accessible spare parts, and engineering decisions that match the actual duty of the facility. The right balance depends on the hoist type, load spectrum, operating environment, and cost of interruption. A lightly used maintenance hoist needs a different plan from a unit supporting continuous manufacturing or dispatch operations.
Establish the Real Causes of Hoist Downtime
Downtime records should distinguish between the immediate fault and the condition that caused it. A contactor may fail, for example, but repeated overheating, contamination, undersized components, excessive starts, or loose electrical connections may be the underlying issue. Replacing the contactor alone restores operation, but it may not prevent another stoppage.
Start by documenting every event: date, equipment identification, operating condition, fault symptom, corrective action, parts used, and hours lost. Over several months, this record reveals patterns that are easy to miss when incidents are handled individually. A recurring pendant cable fault, brake adjustment issue, limit switch trip, or rope wear concern deserves a permanent corrective action rather than another temporary repair.
It also helps to separate planned downtime from unplanned downtime. A controlled service window is normally far less costly than a failure during a critical shift. The goal is not to eliminate all maintenance stoppages. It is to replace unpredictable interruptions with short, planned interventions that protect safety and equipment life.
How to Reduce Hoist Downtime With Planned Maintenance
Planned maintenance should follow the equipment manufacturer’s requirements while reflecting actual site conditions. Hoists operating near capacity, making frequent starts and stops, or working in heat, dust, humidity, chemical exposure, or outdoor conditions need closer attention than equipment in clean, low-duty service.
A practical program has three levels. Operators carry out pre-use observations. Site maintenance personnel perform routine scheduled checks and basic servicing. Qualified lifting-equipment technicians complete periodic detailed inspections, measurements, adjustments, and functional tests. Each level has a clear purpose, and none replaces the other.
Focus on the components that stop production
The most common downtime drivers are often visible before complete failure. Brakes may become noisy, slip, drag, or show abnormal wear. Wire ropes can develop broken wires, corrosion, kinking, crushing, or uneven winding. Chain can elongate or wear at contact points. Electrical systems may show damaged cables, loose terminals, worn contactors, overloaded controls, or inconsistent pendant response.
Travel mechanisms also deserve attention. Misaligned runway rails, worn wheels, inadequate lubrication, damaged buffers, and poor end-stop conditions can place additional stress on the hoist and crane. A hoist may appear to have an electrical fault when the real problem is mechanical resistance in the movement system.
Scheduled servicing should include cleaning, lubrication where specified, fastener checks, brake assessment, electrical inspection, limit-switch testing, and verification of control functions. It should also confirm that warning labels, load markings, hooks, latches, and safety devices remain usable and legible. Maintenance findings must be recorded, including measurements and parts approaching replacement limits.
Plan work around operating demand
The maintenance schedule needs to fit the production calendar. Servicing a high-use hoist during a planned line changeover or low-demand period reduces disruption and makes it easier to perform a complete inspection. Deferring a known issue because the unit is busy usually shifts the disruption to a less convenient time.
For critical lifting points, consider condition-based triggers in addition to calendar intervals. An increase in brake adjustment frequency, repeated electrical trips, abnormal motor temperature, or a rising number of operator reports can justify early intervention. This is especially valuable where failure would stop an entire process rather than one local work area.
Make Operators Part of the Reliability Plan
Operators are the first people to notice changes in hoist behavior. Their daily checks do not need to be complicated, but they must be consistent. Before use, the operator should look for visible damage, test the pendant and directional controls, confirm brake holding performance, observe hook and latch condition, and listen for unusual noise during lifting and travel.
Training should explain why these checks matter and what requires the hoist to be removed from service. Operators need to recognize signs such as jerky movement, delayed brake response, repeated overload activation, rope defects, a hook that will not rotate freely, or control buttons that stick. Reporting a small symptom early is a professional operational decision, not an inconvenience.
Operating practice has a direct effect on service life. Side pulling, shock loading, lifting beyond rated capacity, dragging loads, rapid reversing, and allowing rope to wind poorly on the drum can damage components quickly. The same applies when a hoist is selected for occasional lifting but is used as a high-cycle production device. Good operator training protects both uptime and people working around the load.
Keep Critical Spare Parts Available
A well-maintained hoist can still experience an unexpected component failure. The difference between a two-hour repair and a multi-day outage is often whether the correct part is available. Spare-parts planning should be based on equipment criticality, lead time, failure history, and compatibility with the installed model.
For a critical hoist, facilities commonly review stock for items such as contactors, control fuses, pendant components, limit switches, brake parts, wire rope or chain assemblies, hook latches, and selected bearings. The exact list depends on the make, model, duty class, and age of the equipment. Stocking every possible part is not commercially sensible, but relying on emergency sourcing for high-risk items can be equally expensive.
Part identification is essential. Keep accurate equipment records with serial numbers, capacity, hoist configuration, motor and control specifications, rope details, and previous replacement history. Generic descriptions can lead to ordering errors, particularly where a system has been modified or custom-engineered for a site.
MFEI supports this planning through locally available spare parts and technical assessment, helping facilities identify the items that justify holding on site versus those that can be supplied through a planned service arrangement.
Check Whether the Hoist Still Fits the Application
Repeated faults may signal a design mismatch rather than poor maintenance. A hoist selected at the minimum required capacity can be unsuitable if the application involves frequent near-rated loads, long lifts, high duty cycles, poor power quality, or demanding environmental conditions. Likewise, a standard arrangement may struggle where headroom, travel path, load control, or access for maintenance was not properly considered.
Review the application when downtime becomes repetitive. Consider the average and maximum load, lifts per hour, lifting height, travel distance, start-stop frequency, required positioning accuracy, and ambient conditions. Examine whether the load is stable and centered, whether operators have clear sight lines, and whether the unit can be safely accessed for inspection and repair.
In some cases, a targeted upgrade is more cost-effective than repeated repairs. This could mean a higher-duty hoist, improved controls, a better pendant arrangement, a variable-frequency drive for controlled movement, upgraded braking, or changes to the supporting crane and runway. The right decision depends on the cost of downtime, not only the price of the replacement component.
Build a Clear Response Process for Faults
When a hoist stops, response time depends on clarity. Operators should know who to notify, what information to provide, and how to isolate the equipment safely. Maintenance teams should have access to service history, wiring information, spare-part records, and an escalation route for specialist support.
Avoid returning equipment to service based only on the disappearance of a symptom. After repair, verify the function that failed and assess related components. If an overload device trips repeatedly, for instance, investigate actual load weight, lifting practice, mechanical resistance, and electrical supply conditions before resetting the system and moving on.
For facilities with several lifting assets, a simple monthly review of outage hours, recurring faults, overdue inspections, and parts consumption can guide maintenance priorities. This turns reliability from a reactive maintenance issue into an operational management practice.
A dependable hoist is built through ordinary disciplines performed consistently: correct use, timely inspection, fit-for-purpose engineering, and fast access to knowledgeable support when conditions change. Start with the hoist that would cause the greatest disruption if it failed tomorrow, then give it the maintenance attention and parts strategy its role in your operation deserves.