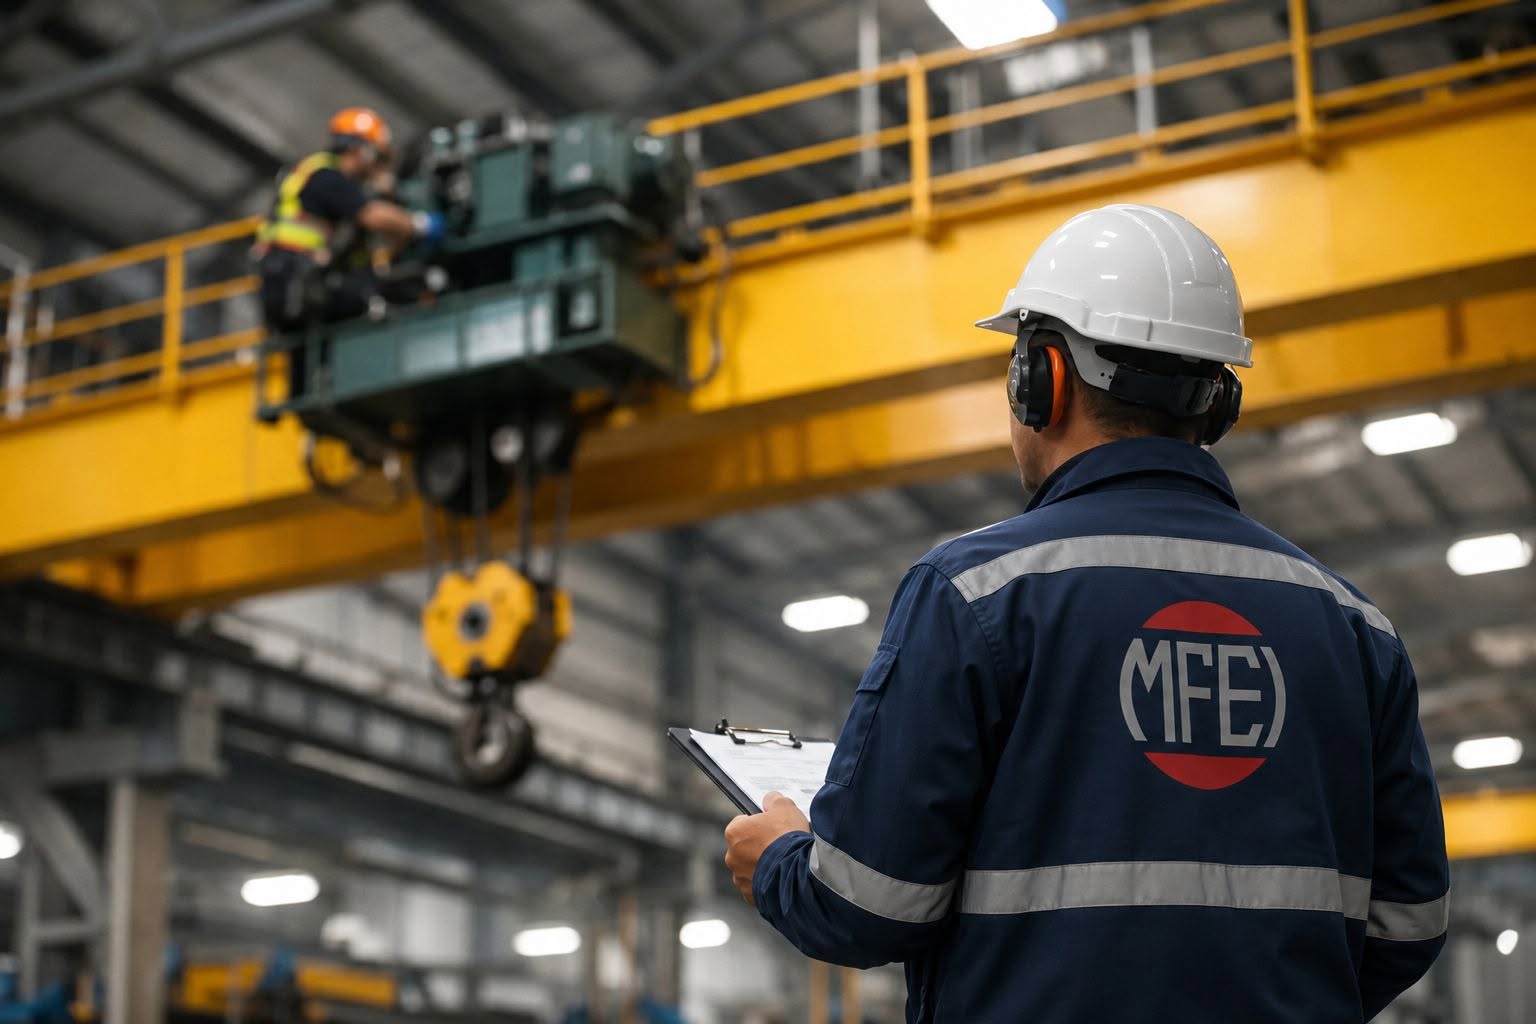
A crane can appear to be operating normally right up to the point it causes a production stoppage. A worn hoist brake, damaged wire rope, misaligned runway, or intermittent pendant control may not be obvious during routine lifting, yet each can quickly turn into a safety concern and an expensive disruption. Effective bridge crane maintenance is therefore not a repair activity to schedule after a failure. It is a planned engineering discipline that protects people, load-handling capacity, and plant uptime.
For plant managers and maintenance teams, the objective is practical: keep the crane safe, available, and suited to the work it performs. That requires more than a quick visual check. It requires inspections at the right intervals, records that reveal recurring faults, qualified service personnel, and ready access to appropriate spare parts.
Why bridge crane maintenance affects more than the crane
An overhead bridge crane is part of the wider production system. When it cannot lift, position, or transfer materials, downstream work may stop even if every other machine remains available. In fabrication, manufacturing, warehousing, and maintenance workshops, an unplanned crane outage can delay dispatches, extend shutdown work, and create unsafe manual handling workarounds.
Maintenance also has a direct effect on equipment life. A small problem in a limit switch or contactor may be inexpensive to correct. Left unattended, it can contribute to overtravel, load sway, motor stress, or damage to other components. The cost of corrective work is not just the replacement part. It includes lost operating time, emergency labor, inspection requirements, and the risk of a load-handling incident.
The right service program balances reliability with cost discipline. Not every crane needs the same maintenance frequency or scope. A low-duty crane used occasionally in a controlled workshop has different needs from a crane operating multiple shifts in a dusty, humid, hot, or corrosive environment. Service planning should reflect actual duty cycle, load spectrum, operating conditions, equipment age, and the consequences of downtime.
What a bridge crane maintenance program should cover
A useful maintenance program separates routine operator observations from periodic technical inspections and planned servicing. Operators are often first to notice changes in crane behavior, while trained technicians are responsible for assessing safety-critical components, electrical condition, mechanical wear, and compliance with the manufacturer’s requirements.
Daily and pre-use observations
Before operation, the person using the crane should look for visible damage, unusual conditions, and changes in normal behavior. This does not replace a formal inspection, but it can prevent a known defect from becoming an incident during the shift.
The operator should confirm that the pendant or radio controls respond correctly, emergency stop functions as intended, and the hook, latch, and load chain or wire rope show no visible damage. They should also listen for unusual noise from the hoist, trolley, or bridge travel drives. Jerky movement, excessive vibration, poor braking, unusual sparks, or a burning smell should be treated as a reason to stop operation and report the crane.
A simple reporting route matters. If operators believe a small fault will be ignored or will complicate production targets, defects go unreported. Clear tag-out procedures and responsive maintenance support encourage early intervention, which is almost always less disruptive than emergency repair.
Periodic mechanical inspection
The hoist assembly deserves close attention because it carries the load directly. Technicians should inspect the hook for deformation, cracks, excessive throat opening, twisting, and latch condition. Wire rope requires checks for broken wires, corrosion, crushing, kinks, poor spooling, and lubrication condition. For chain hoists, wear, elongation, lubrication, and seating on the sprocket are central concerns.
Brakes should be tested for reliable holding and controlled stopping. A brake that slips or responds inconsistently is a high-priority defect. Couplings, gearboxes, bearings, shafts, wheels, and travel drives should also be checked for wear, alignment, lubrication, and abnormal noise.
The bridge structure and trolley frame need examination for loose fasteners, damage, corrosion, and signs of fatigue. Runway rails, end stops, buffers, and collector systems should not be overlooked. Crane performance can be affected by track alignment or wheel wear long before a dramatic travel fault occurs.
Electrical and control inspection
Electrical problems often begin intermittently. A crane may lose motion only at certain positions on the runway, experience erratic speed control, or trip protection devices without an obvious cause. These symptoms should be investigated rather than repeatedly reset.
Periodic servicing should include inspection of control panels, contactors, relays, variable-speed drives where fitted, cable festoon systems, pendant stations, radio controls, limit switches, and earthing arrangements. Loose terminals, heat discoloration, moisture ingress, damaged insulation, and worn cable carriers can lead to unpredictable operation or component failure.
For older cranes, control modernization may be more cost-effective than repeatedly addressing obsolete electrical components. This decision depends on the condition of the mechanical structure, availability of parts, expected future duty, and whether the upgraded controls can improve positioning, diagnostics, or safety functions.
Set maintenance intervals around real operating conditions
Calendar-based maintenance provides a starting point, but hours of use and service conditions should shape the final plan. A crane used for short, light lifts once a week may need a different inspection rhythm than one lifting near its rated capacity every day. High-duty applications, outdoor installations, abrasive dust, chemical exposure, and frequent starts and stops all accelerate wear.
Maintenance records help make this judgment evidence-based. Record service dates, observed defects, parts replaced, brake adjustments, rope measurements, electrical test results, and breakdown history. Over time, these records reveal patterns. If a particular contactor fails repeatedly, the issue may be excessive switching duty, inadequate enclosure protection, or an underlying motor problem rather than the contactor itself.
Planned service should be coordinated with production requirements. A short scheduled shutdown is usually easier to manage than an emergency stoppage during a critical job. For facilities with a single essential crane, it is sensible to identify the components with the greatest effect on availability and maintain a practical stock of critical spares.
Spare parts are part of the uptime strategy
A maintenance plan is only as effective as the parts support behind it. Keeping every possible component on site ties up capital and can create storage issues. Keeping nothing on hand can turn a minor fault into days of lost production. The appropriate approach is to assess lead time, failure history, equipment criticality, and the availability of a backup lifting method.
Common critical items may include contactors, overload protection components, limit switches, pendant assemblies, brake parts, wire rope or chain, hook latches, and selected bearings or wheels. The exact list should be based on the installed crane configuration, not a generic inventory sheet.
Parts must also be correct for the equipment. Substituting an unsuitable brake component, wire rope specification, electrical device, or hook assembly can compromise performance and safety. Experienced crane technicians can verify compatibility and determine whether a replacement is sufficient or whether a wider repair is needed.
When repair is no longer the best answer
There is a point where repeated repairs are not the most economical choice. This does not automatically mean replacing the whole crane. A targeted modernization may extend useful life by upgrading controls, replacing the hoist, improving power supply arrangements, or addressing runway condition.
The decision should consider total operating cost, not only the immediate repair quotation. Frequent breakdowns, difficult-to-source parts, poor speed control, limited diagnostic capability, and changing load requirements can justify an upgrade. On the other hand, a well-maintained crane with a sound structure and readily available parts may continue to provide dependable service for many years.
A competent assessment should be site-specific. It should account for available headroom, span, lifting height, load capacity, duty classification, operator workflow, and budget. Fit-for-purpose engineering avoids both under-specification and unnecessary spending.
Make maintenance a working partnership
The strongest maintenance arrangements combine site knowledge with specialist lifting expertise. Your operations team understands how the crane is used, where delays occur, and which lifts are critical. A crane service provider brings component knowledge, inspection discipline, repair capability, and access to suitable parts.
For Malaysian facilities, MFEI can support this full lifecycle approach through inspection, maintenance, spare-parts support, and engineering input when a repair, upgrade, or replacement decision is required. The focus should remain on the practical outcome: a lifting system that performs reliably within the demands of the site.
A crane does not need to fail dramatically to deserve attention. Treat unusual movement, changed braking behavior, recurring electrical trips, and visible wear as useful early warnings. Addressed promptly, they help keep the next lift routine, controlled, and safely completed.